
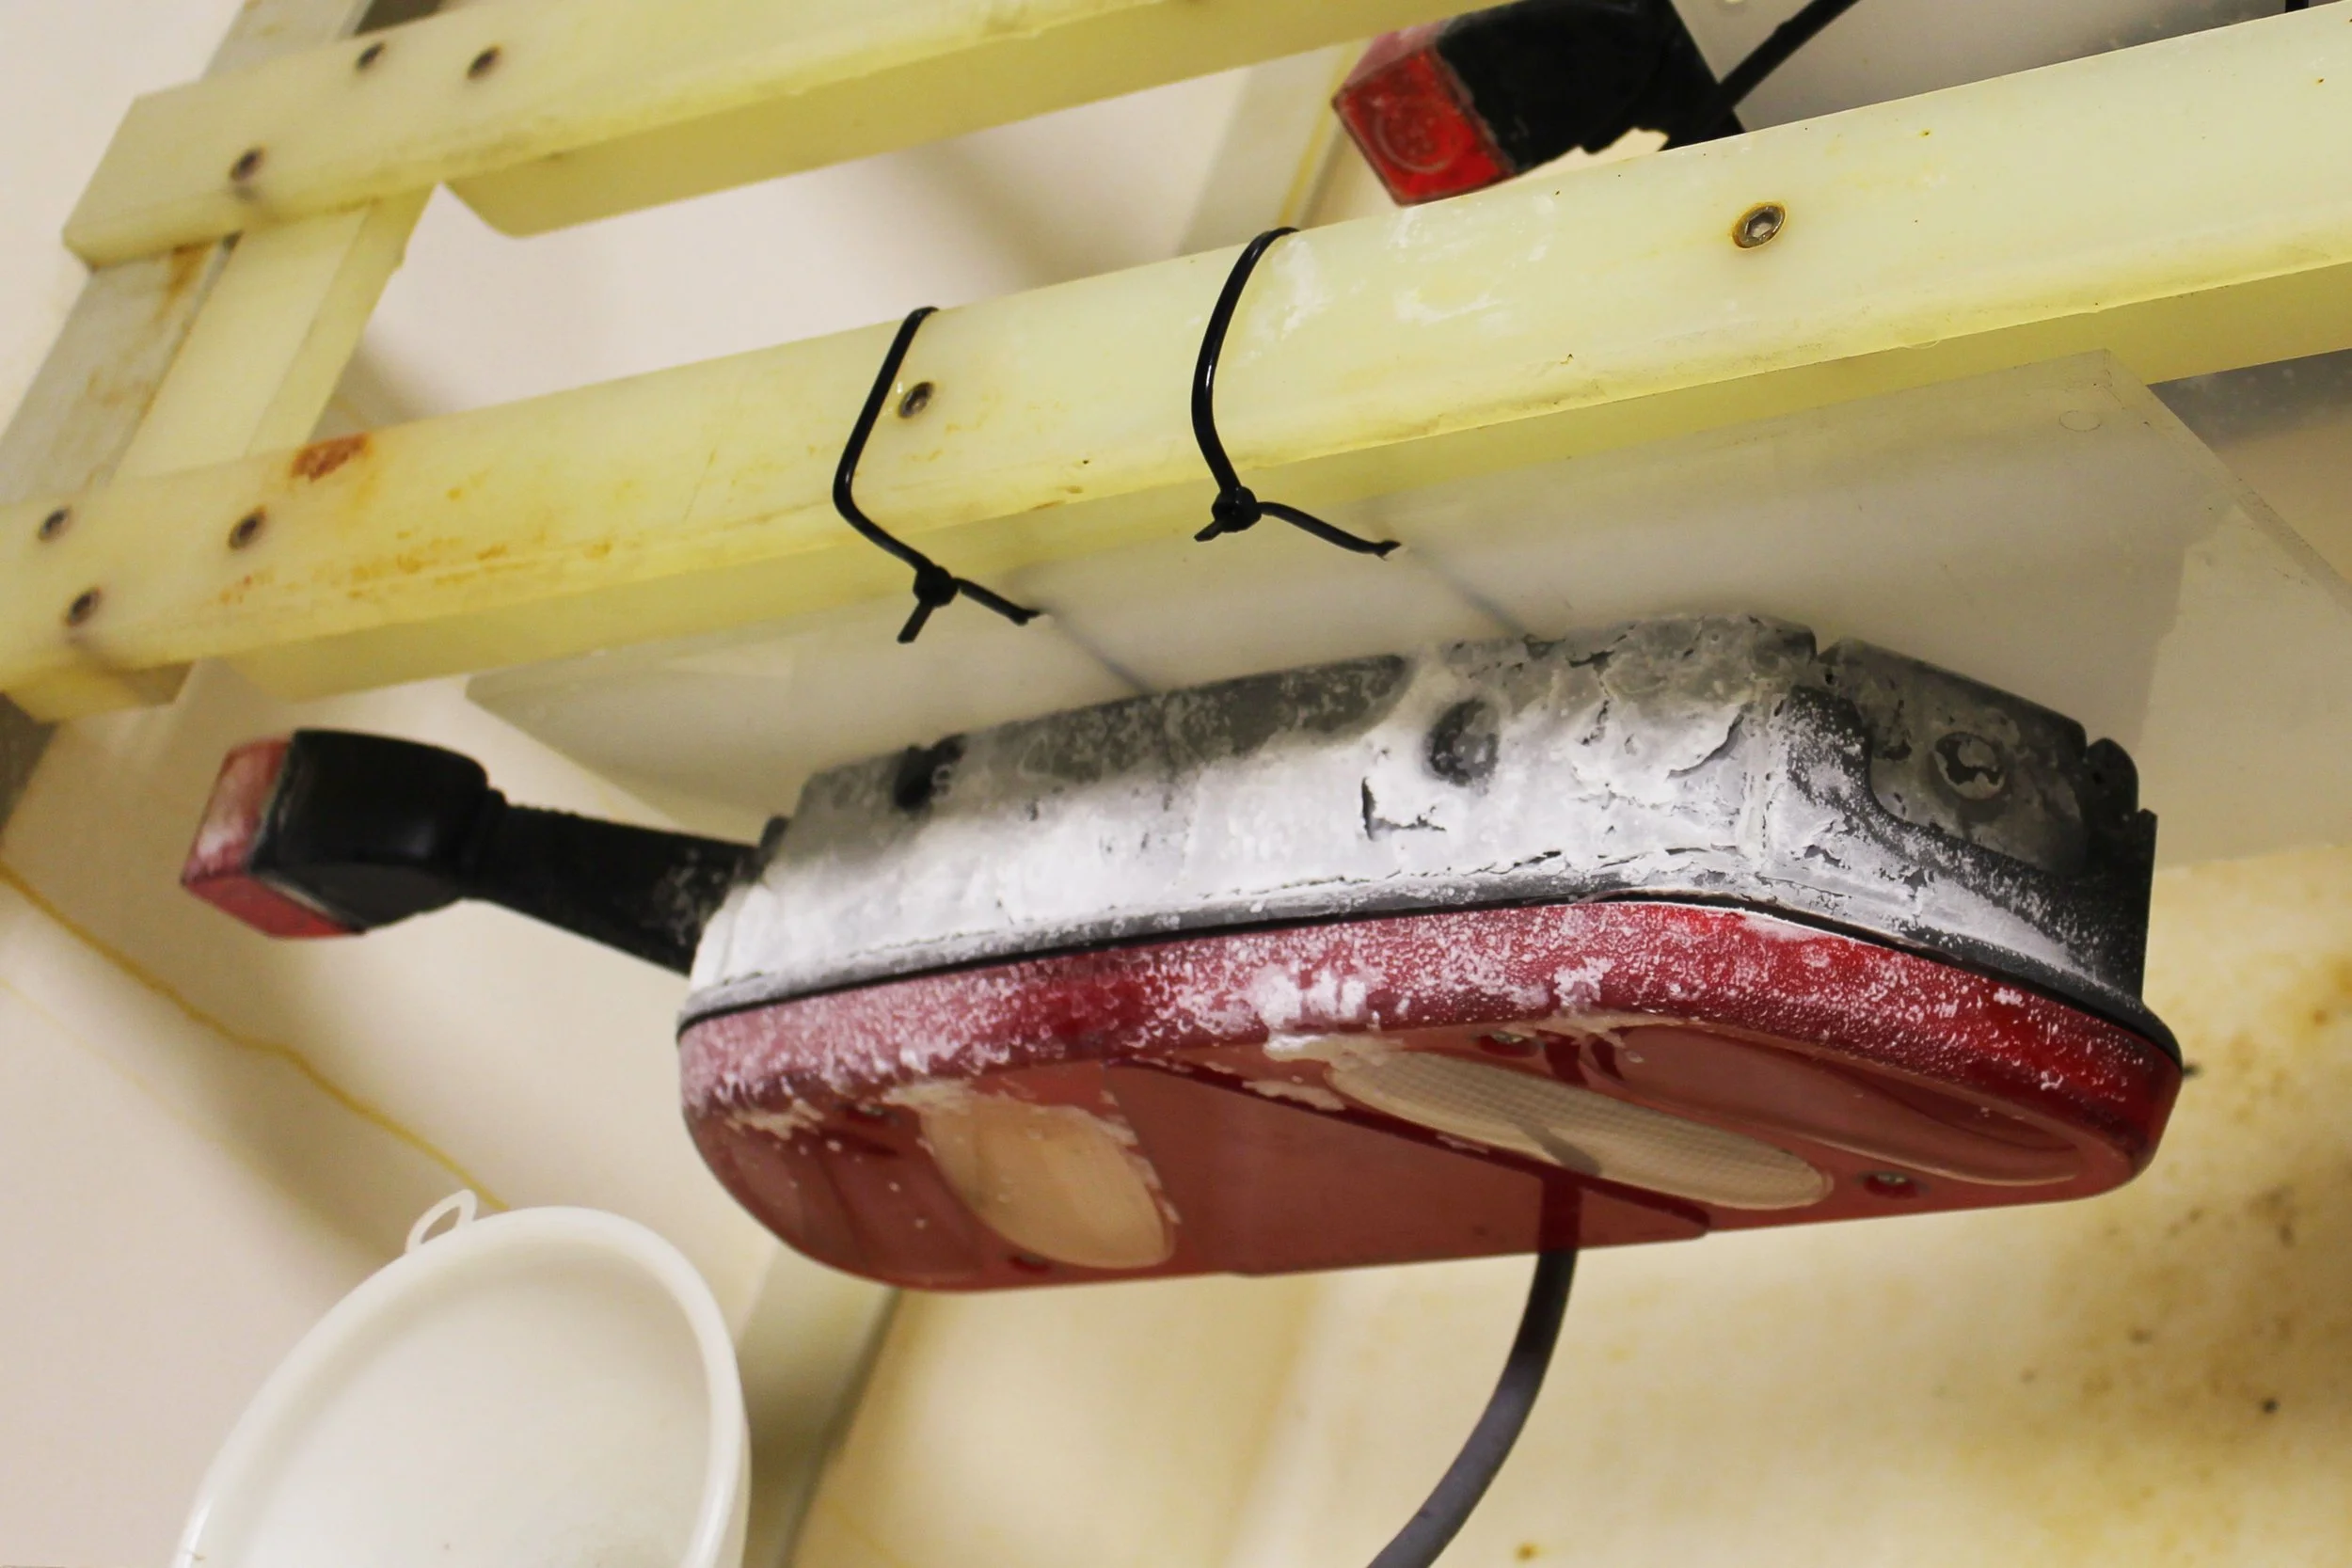
Truck-Lite Europe is marking the first anniversary of its expanded in-house LED lighting testing facility, reinforcing its commitment to product quality, reliability and safety across the commercial vehicle sector.
The investment in advanced testing technology at the company's Harlow facility in Essex provides an additional level of product scrutiny and quality assurance, helping to ensure that Truck-Lite lighting systems meet the demanding operational requirements of commercial vehicle manufacturers, converters and fleet operators.
The facility brings together a comprehensive range of optical, electronic and environmental testing capabilities, allowing Truck-Lite to assess lighting performance, durability and regulatory compliance under conditions designed to replicate those encountered in everyday vehicle operation.
Robert Field, Validation and Legislation Manager at Truck-Lite Europe, explains:
"Our testing facility provides an additional layer of scrutiny and quality assurance throughout the product validation process. It's not simply about demonstrating that a lighting system meets the relevant regulations, but also about understanding how it performs when subjected to the environmental and operational stresses experienced by commercial vehicles.
"By carrying out these demanding tests in-house, we can identify potential weaknesses, verify product performance and maintain greater control over quality. Ultimately, this provides our OEM customers, vehicle converters and fleet operators with further reassurance that the lighting systems they specify are designed and tested for long-term reliability."
Among the facility's key capabilities is a 2,000-hour static LED endurance test, which subjects products to repeated power switching and thermal cycling between +23°C and +60°C. This process assesses electronic and thermal stability over prolonged operating periods.
Environmental testing includes a 96-hour chamber cycle, exposing products to temperatures ranging from –40°C to +60°C and relative humidity levels of up to 95%. Testing can also incorporate vibration to evaluate the combined effects of temperature, moisture and mechanical stress.
Water resistance is assessed through IPX4 spray testing, using 30 rotating water jets and full 360-degree product rotation during one hour of continuous exposure.
The facility also incorporates an optical testing tunnel and reflex testing area, enabling precise measurement of light output, colour accuracy and reflectivity against relevant UN ECE regulatory requirements.
Together, these processes support the validation of printed circuit board assemblies (PCBAs), LED performance and complete lighting systems, while providing valuable data for ongoing product development and quality control.
For commercial vehicle operators, the emphasis on thorough product validation is particularly important. Lighting systems must withstand vibration, road spray, temperature extremes and prolonged use, while maintaining reliable performance and regulatory compliance.